


Titanium Anode OEM Guide for Custom Steel Galvanizing Equipment
If you manage procurement or engineering for a continuous electro-galvanizing line, the anode specification you choose determines coating uniformity, energy cost, and line uptime. This guide covers everything a technical decision-maker needs to know about titanium anode for steel plate galvanizing—from electrochemical fundamentals and material comparisons to OEM customization, supplier evaluation, and maintenance practices. Whether you are retrofitting an existing line or commissioning a new one, the information here will help you make a well-supported sourcing decision.

Understanding Titanium Anodes for Steel Galvanizing
The Electrochemical Role of the Anode
While an electro-galvanizing cell is running, the anode powers the oxygen evolution reaction, which goes from 2 H₂O → O₂↑ + 4H⁺ + 4e⁻. Meanwhile, zinc ions deposit onto the steel strip at the cathode: Zn²⁺ + 2e⁻ → Zn. The anode has to be able to handle high current densities (usually 200–500 A/m²) without changing size, since any change in shape changes the local current density and makes the zinc coating thickness uneven.
Why Dimensional Stability Matters?
A dimensionally stable titanium anode for steel plate galvanizing keeps its shape over the course of its useful life. Traditional lead-silver anodes slowly wear away, changing the space between the electrodes and making the layer less stable. Titanium substrates that have been coated with mixed metal oxides (MMO) don't mix with the electrolyte. The substrate keeps its shape for 10 to 15 years, which is why galvanizing engineers make dimensional stability a must-have requirement.
Operating Conditions and Recommended Current Densities
The current window is controlled by the coating chemistry. Iridium-tantalum (Ir-Ta) coatings work well in liquids that are slightly acidic or alkaline and have a current density of 100 to 400 A/m². In sulfate-acid baths at 300–500 A/m², ruthenium-iridium (Ru-Ir) layers work best. The most important technical choice in anode specification is which coating mixture to use with your electrolyte system. This is also where OEM customization gives you real process value.
Technical Comparison of Anode Materials for Galvanizing Steel Plates
Titanium MMO vs. Lead-Silver Anodes
A lot of years ago, lead-silver anodes were the standard. But they make lead sludge that gets into the zinc bath and costs a lot to get rid of. They are being phased out faster because of pressure from regulators, especially under RoHS and environmental compliance frameworks. Titanium MMO anodes don't pollute with metal, so they don't need to be serviced as often, and they lower the risk of covering flaws caused by metal inclusions.
Titanium MMO vs. Graphite Anodes
When graphite anodes are in acidic zinc sulfate baths, they wear down quickly and lose carbon particles that lower the quality of the deposit. They also have a fairly high oxygen evolution overpotential, which makes the cell voltage higher and uses more energy. On the other hand, titanium anodes with Ru-Ir layers have a much smaller overpotential, which means they use less power per unit of zinc they deposit. It has been shown in published electrochemical data that switching from graphite to MMO titanium saves between 10 and 20 percent of energy.
Lifecycle Cost Analysis
MMO titanium anodes cost more up front than graphite or lead alternatives, but over a 10-year period, titanium is cheaper to own overall. Because titanium surfaces can be cleaned and recoated, they don't need to be completely replaced every time they need to be maintained. When you add in less energy use, lower costs for bath pollution, and longer breaks between planned downtimes, titanium makes a clear financial case for any high-volume galvanizing business.
Custom OEM Titanium Anode Solutions for Steel Plate Galvanizing
Tailored Dimensions and Coating Selection
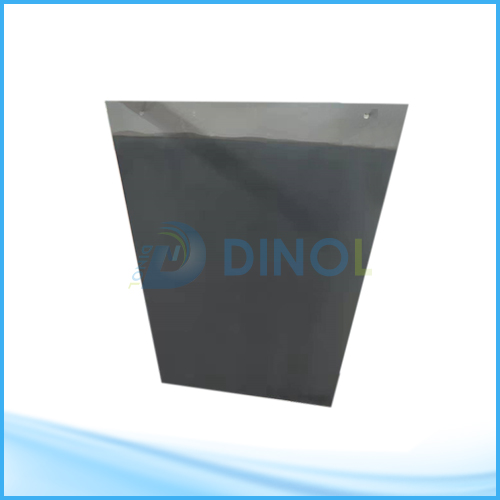
There are no two galvanizing lines that have the same cell geometry or electrolyte chemistry. Shaanxi Tianyi makes custom titanium anodes that match the line designer's exact drawing tolerances for busbar connection points, inter-electrode spacing, and plate or mesh configurations. Coatings are chosen based on the chemistry of the process: Ir-Ta is used in mildly acidic or alkaline baths, Ru-Ir is used in sulfate-acid systems, and PbO₂ variants are used when the chemistry of the bath calls for them. Titanium substrates come in Grade 1 or Grade 2, and niobium can be used for high-voltage uses.
These are the main quality checks that are done on every custom order:
- XRF Coating Thickness Measurement — Confirms MMO loading uniformity across the active surface to ensure consistent current distribution from day one.
- Accelerated Life Testing (ALT) — Conducted per NACE TM0294 protocols, predicting long-term coating durability under production-equivalent current densities.
- SEM Morphology Analysis — Detects micro-cracks or porosity before shipment, preventing premature substrate passivation on the line.
- Thermal Shock Adhesion Testing — Thermal cycling to 500 °C followed by water quenching verifies that the coating will not delaminate under high-current thermal stress.
- Dimensional Tolerance Verification — Each anode is checked against the customer's drawing to confirm busbar and cell fitment.
The main worry of galvanizing engineers is that a single failed anode could cause uneven zinc coating, which would lead to a batch quality incident. At Tianyi, passing all five checks before sending something out is required, not just an extra.
OEM/ODM Certification and Confidentiality
The plans and process settings for the steel plant are secret. Tianyi follows strict NDA rules, and titanium anode for steel plate galvanizing shape data that is unique to each customer is never shared or used for something else. OEM and ODM projects are overseen by engineers who make sure the drawings are correct, make samples, and make sure that price trials are coordinated within the time frame set by the customer.
Procurement Guide: Sourcing Titanium Anodes for Galvanizing Equipment
Evaluating Supplier Credentials
A good titanium anode for steel plate galvanizing supplier should give you polarization curves, ALT reports, and data on how well the coating sticks to the electrolyte system you use. References from galvanizing lines that are similar, ideally with similar current levels and strip widths, are more reliable than general approvals. Ask the seller if they have worked with ongoing EG lines that handle a million tons of EG per year.
Lead Times and Annual Maintenance Windows
Most big galvanizing lines have planned outages every year that last between 7 and 15 days. Anode delivery has to perfectly match this window; any delays that last more than a few days cause production to drop. Find out how long it takes for the supplier to make custom orders (usually 4–8 weeks for a full cell set), and add extra time to your procurement schedule just in case. Tianyi keeps up a production capacity that is set up to meet the needs of urgent custom orders.
After-Sales Support and Warranty
Reliable customer service after the sale is a buying factor that is often overlooked in favor of price. If there are problems with anode performance, they need to be found quickly. You should expect remote technical support within 24 hours and on-site availability within 48 hours at the very least. When you combine warranty terms that cover coating performance under certain working conditions with base recoating services, you can protect your capital investment for the entire life of the anode.
Maximizing the Performance and Lifespan of Titanium Anodes
Routine Inspection and Cleaning Schedules
Visual inspections and impedance checks done on a regular basis can help find early signs of covering wear on a titanium anode for steel plate galvanizing before they affect the quality of the zinc layer. At each scheduled repair window, use a weak acid rinse to clean the anode surfaces and get rid of the zinc oxide scale. Then, look for patterns of discoloration that show where the coating is wearing away. Record measurements of the gap between the electrodes at every power outage to make sure that the dimensions stay the same over time.
Recognizing Early Failure Indicators
One of the first signs that a covering is almost done is a rise in cell voltage at steady current density. Coating weight gages can find that the zinc thickness isn't the same across the width of the strip. This is usually caused by localized anode surface degradation. If you notice these signs early, you can plan to coat the lines again during the next planned outage instead of having to stop the line without warning.
Environmental and Sustainability Benefits
Titanium MMO anodes are more in line with goals for environmentally friendly manufacturing than older materials. They completely get rid of the production of lead sludge, use less energy because they lower the oxygen evolution overpotential, and their reuse substrates cut down on metal waste over the span of the equipment. The move to MMO titanium anodes makes a measurable difference in lowering hazardous waste levels and making activities more compliant with environmental laws.
Conclusion
Choosing the right anode standard for a continuous electro-galvanizing line is a choice that will have effects for a long time. A titanium anode for steel plate galvanizing is better than lead-silver and graphite alternatives when it comes to resistance to corrosion, stability in size, energy efficiency, and environmental friendliness. Custom OEM solutions that are made to fit your cell's shape, electrolyte chemistry, and current density range give you more consistent zinc coating and longer service intervals. The qualities of the seller that protect your production investment over the full anode service life are strict quality control before shipment, on-time delivery that fits with maintenance windows, and quick support after the sale.
FAQ
How long do titanium anodes typically last in an electro-galvanizing line?
With proper operating conditions and periodic maintenance, MMO-coated titanium anodes deliver 10–15 years of service life. The titanium substrate is reusable—it can be stripped and recoated at end-of-coating-life, extending the asset's total lifespan well beyond that of graphite or lead-silver alternatives.
What coating should I specify for a sulfate-acid zinc bath?
Ruthenium-iridium (Ru-Ir) coatings are the standard recommendation for sulfate-acid electrolyte systems operating at 300–500 A/m². For alkaline or mildly acidic baths, iridium-tantalum (Ir-Ta) coatings are preferred. The correct match between coating chemistry and electrolyte type is critical for achieving rated service life.
Can dimensions and connection hardware be fully customized?
Yes. Tianyi engineers anodes to customer drawings, including plate or mesh geometry, thickness, busbar connection points, and installation hardware. All dimensional data is handled under confidentiality agreements.
What quality documentation is provided with each order?
Standard documentation includes XRF coating thickness reports, ALT test results, SEM morphology analysis, adhesion test records, and dimensional inspection certificates referenced to the customer's drawing revision.
Partner with Tianyi for Custom Titanium Anode for Steel Plate Galvanizing Manufacturer Solutions
Every OEM project that Tianyi works on is backed by proven electrochemical engineering experience. Our custom MMO titanium anodes are made to your exact line specifications, including the coating chemistry, substrate grade, geometry, and connection hardware. They are also tested for quality before they are shipped. We can help you set up an annual repair window and respond to your technical questions within 24 hours if you need us to. To get a technical advice or project price, email our engineering team at info@di-nol.com.
References
1.Trasatti, S. (1999). Electrochimica Acta— Electrocatalysis: Understanding the success of DSA.
2.Beer, H. B. (1980). Journal of the Electrochemical Society— The invention and industrial development of metal anodes.
3.Comninellis, C., & Vercesi, G. P. (1991). Journal of Applied Electrochemistry— Characterization of DSA-type oxygen-evolving electrodes.
4.Lipp, L., & Pletcher, D. (1997). Electrochimica Acta— The preparation and characterization of tin dioxide-based coatings on titanium.
5.NACE International. (2005). NACE TM0294— Testing of embossed metallic coated steel sheet.
6.Chen, G. (2004). Separation and Purification Technology— Electrochemical technologies in wastewater treatment — includes comparative anode performance data relevant to galvanizing applications.